
Pressure pipe performance depends on more than the strength of polyethylene resin. Wall thickness must remain within specified limits along the entire pipe length, because local variations can affect pressure resistance, material use, and dimensional compliance. The Standard Dimension Ratio (SDR), calculated by dividing nominal outside diameter by nominal wall thickness, provides a common way to relate pipe dimensions to pressure design.
A PE plastic extruder machine must maintain a stable flow of molten polymer while downstream equipment controls the pipe’s dimensions and movement. Achieving consistency requires coordinated adjustments to die geometry, haul-off speed, cooling, and measurement rather than relying on a single machine setting. DEKUMA manufactures polyethylene pipe extrusion equipment used in industrial pipe production.
Understanding SDR and the Sources of Wall Variation
SDR links a pipe’s outside diameter to its nominal wall thickness. For a given nominal diameter, a lower SDR corresponds to a thicker wall, while a higher SDR indicates a thinner wall. This relationship helps engineers compare pipe dimensions, but the specified SDR alone does not describe every aspect of pressure performance. Material grade, applicable standards, operating temperature, and service conditions also influence the pipe’s permitted use.
Wall variation can originate at several points in the extrusion process. Uneven melt distribution around the die circumference may produce thick and thin sectors, while fluctuations in output can alter the amount of polymer delivered per unit of pipe length. Downstream movement introduces another variable: if the haul-off speed changes while output remains constant, the mass of material deposited along each metre of pipe also changes. Cooling and sizing conditions can further influence the final dimensions.
These variables interact rather than operate independently. A small change in melt temperature may affect viscosity and flow through the die; a change in haul-off speed can alter both wall formation and production rate. Operators need to distinguish circumferential variation from variation along the pipe length, since the two patterns may have different causes. Establishing a reliable baseline for output, temperature, pressure, and line speed gives production teams a reference for diagnosing deviations.
Coordinating Die Gap, Output, and Haul-Off Speed
The die head distributes molten polyethylene into an annular shape before the pipe enters the sizing and cooling section. Its gap, alignment, and flow-channel geometry influence how evenly material exits around the circumference. If the gap is uneven or the flow is poorly balanced, one side of the pipe may become thicker than the other even when average wall thickness appears acceptable. Die adjustments must account for the resin’s rheological behaviour and the intended pipe dimensions.
Output and haul-off speed determine how much material forms each unit of pipe length. Increasing output without adjusting line speed generally adds more material per metre, while increasing haul-off speed at unchanged output tends to reduce it. These relationships provide useful process controls, but corrections should be gradual because changes can affect pipe diameter, cooling behaviour, and the stability of the downstream sizing system. Operators must also allow for the delay between an adjustment and the point where its effect becomes measurable.
A PE extruder needs to operate as part of a coordinated production line. Screw speed, melt temperature, die pressure, haul-off speed, and cooling conditions should be monitored together instead of being adjusted in isolation. Stable feed and melt delivery help limit output fluctuations, while a consistent haul-off rate reduces longitudinal variation. Documented operating windows for each pipe specification can shorten setup time and make production changes more repeatable between shifts.
Vacuum Calibration and In-Line Measurement
After leaving the die, hot polyethylene must be sized and cooled while retaining its intended geometry. Vacuum calibration draws the pipe against a sizing sleeve, helping control outside diameter during the early stages of solidification. Cooling-water distribution and temperature also matter: uneven cooling may cause dimensional instability or residual stress, particularly when the pipe wall is thick or the production rate is high.
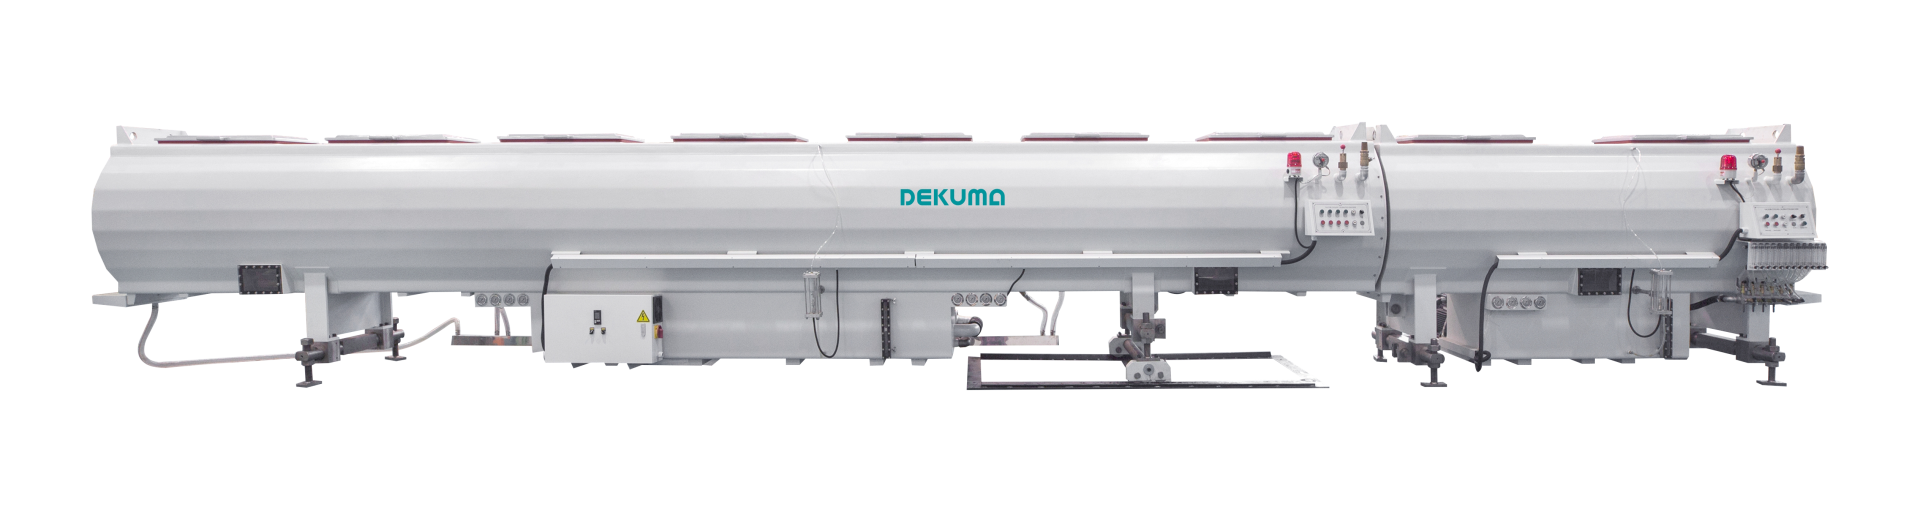
The equipment configuration supplied for DEKUMA includes a stainless-steel vacuum calibration tank and piping, a dual water-circulation system with independent filters, responsive vacuum control, and automatic water-temperature and level control. Single- or double-chamber configurations are available according to production requirements. These features are relevant to dimensional stability because consistent vacuum and cooling conditions help maintain the pipe’s shape during sizing. They do not, by themselves, measure wall thickness or establish SDR compliance; the full line must be configured and validated for the target pipe specification.
In-line measurement adds information that visual inspection cannot provide. Depending on the system, ultrasonic or other suitable measurement technology can assess wall thickness at multiple circumferential positions as the pipe moves through production. Data can reveal whether the average wall is drifting, whether one sector remains consistently thin, or whether fluctuations occur at intervals along the length. Measurement accuracy depends on sensor configuration, calibration, material properties, pipe geometry, and the measurement method used.
The most useful monitoring arrangement connects measurement results with a defined correction procedure. If average thickness declines, output or haul-off speed may require adjustment; if the wall is uneven around the circumference, die alignment or local flow distribution may need investigation. Because the measurement point lies downstream of the die, the detected section may already have travelled some distance before a correction takes effect.
Conclusion
Consistent SDR wall thickness emerges from the relationship between material flow, die geometry, line speed, and downstream dimensional control. A PE plastic extruder machine supplies the molten polymer, but reliable pressure-pipe production depends on the entire line maintaining stable conditions and detecting deviations early.
Vacuum calibration supports outside-diameter control, while circumferential and longitudinal measurements reveal variations that average readings can conceal. Production teams should validate settings against the applicable pipe standard, verify measurement equipment, and confirm minimum wall thickness through appropriate inspection. DEKUMA supplies extrusion and calibration equipment for polyethylene pipe manufacturing, while final compliance depends on application-specific configuration, process validation, and documented product testing.
